
 中文简体
 English
 русский
 عربى

A production manager comparing quotes for a Horizontal Metal Band Saw Machine usually starts with the capacity line: 500 mm round, 500 × 700 mm rectangle. What that line does not say is how many bars the machine will get through in a shift. A saw of this type works through steel by area, so the time for one cut is roughly the cross-section divided by the cutting rate, and a buyer can check how many machines the shop really needs before the order is placed.
Cross-Section Area Sets Cut Time
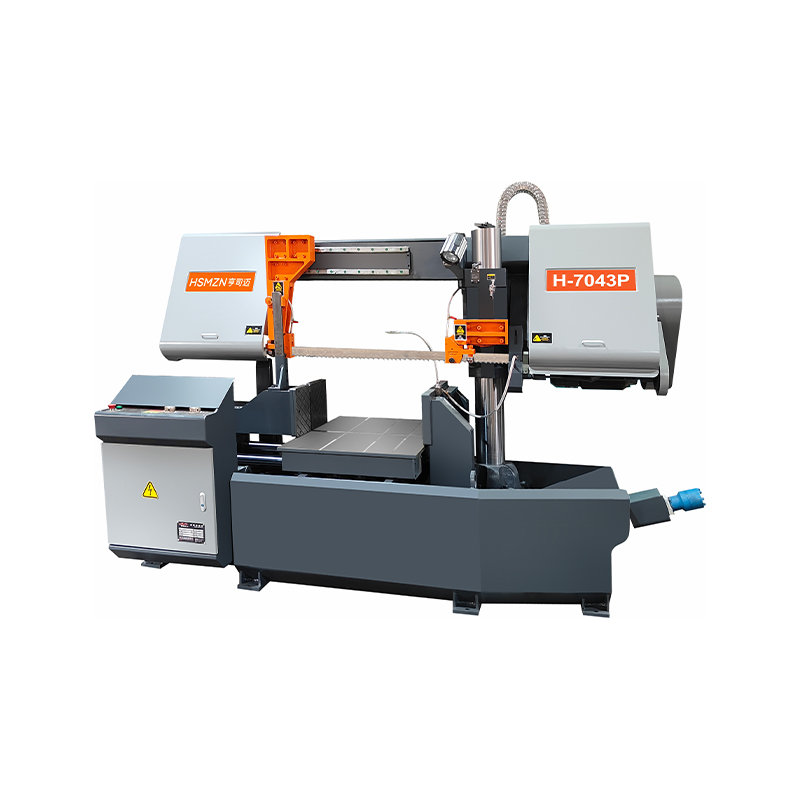
The H-7050P double column model from Zhejiang Hengsimai Intelligent Machinery, a maker of sawing equipment for more than 30 years, cuts round bar up to 500 mm in diameter and rectangular sections up to 500 × 700 mm. Those two limits describe very different amounts of steel: 500 mm round is about 1,964 cm², while 500 × 700 mm is 3,500 cm². The table below uses two assumed cutting rates, 100 and 150 cm² per minute, as an illustration for mild steel. Actual rates depend on the material, the blade, and the feed setting.
|
Section |
Area |
Time at 100 cm²/min |
Time at 150 cm²/min |
|
Round, 300 mm |
707 cm² |
about 7 min |
about 5 min |
|
Round, 500 mm |
1,964 cm² |
about 20 min |
about 13 min |
|
Rectangle, 500 × 700 mm |
3,500 cm² |
35 min |
about 23 min |
A shop that cuts twelve 300 mm blanks a day needs about 85 minutes of sawing at the slower rate, so one saw has plenty of spare time. Thirty 500 mm bars a day is a different case: about 588 minutes, nearly ten hours. A common planning assumption is to leave a quarter of a shift for loading, blade changes and upkeep, which leaves about 360 minutes of sawing in an eight-hour shift. Even at 150 cm² per minute, the thirty bars need about 393 minutes, so the shop needs a second saw, a second shift, or a faster cutting rate. A Horizontal Metal Band Saw Machine sized for 500 × 700 mm sections is a different investment from one sized for 300 mm bar, and the table shows why.
Blade Speed From 14 to 70 m/min
The model runs at a process speed of 14 to 70 m/min with a 41 × 1.3 × 5450 mm blade. At 14 m/min the 5.45 m blade loop passes the cut about 2.6 times a minute; at 70 m/min about 12.8 times. The slow end suits stainless steel, tool steel and very large sections, where heat builds quickly, and the fast end suits softer materials such as aluminium. Variable blade speed through an inverter is an option, and automatic blade speed monitoring is listed as a standard feature. The inverter option is worth fitting when one saw has to cut both stainless steel and aluminium. A wide 41 mm blade resists twisting in a deep cut, which keeps a horizontal metal band saw cutting straight through a 500 mm section. Choosing the speed range is part of specifying a Horizontal Metal Band Saw Machine for a given mix of materials.
Power and Floor Space
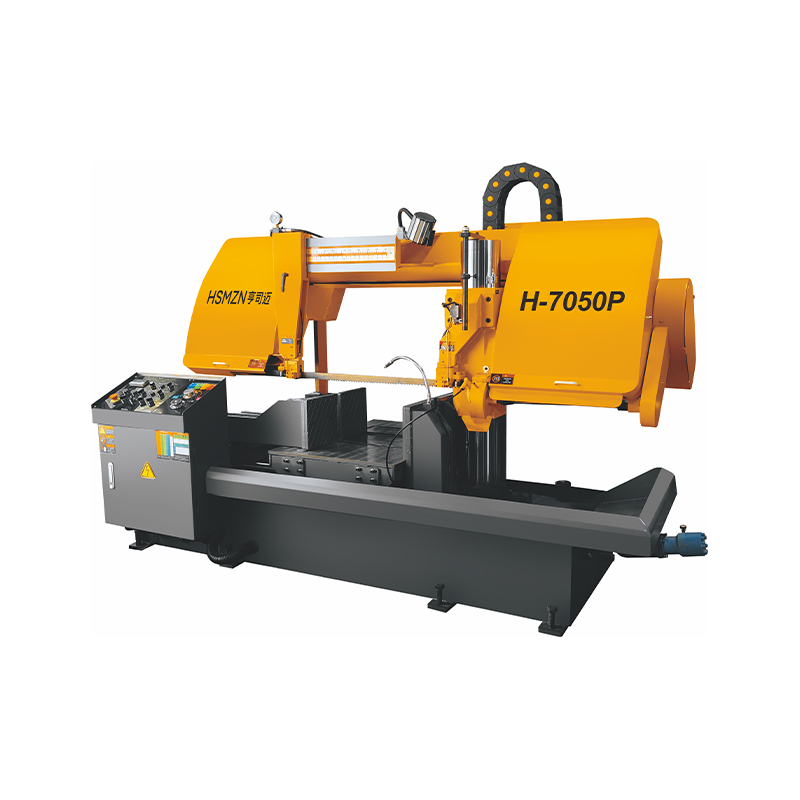
The main motor is 7.5 kW with four poles, supported by a 1.5 kW oil pump and a 0.12 kW coolant motor, and both clamping and blade tensioning are hydraulic. The machine measures 2950 × 2670 × 1950 mm, but the floor space needed is longer than that. A 6 m bar needs roughly 6 m of roller table on the infeed side, and the cut piece needs room on the other. Roller tables can be made to the bar length in use. Planners who count only the machine footprint often find the bay too short, so Horizontal Metal Band Saw Machines are placed along a wall with the full bar length clear. The bay should be checked against the length of the bar, not against the footprint of the Horizontal Metal Band Saw Machine.
Long Cuts Free the Operator
A 20 to 35 minute cut leaves an operator with little to do once the bar is clamped and the length is set. On a semi-automatic band saw machine, the operator loads the bar, sets the length on the digital display (0.1 mm step), and starts the cut. Many workshops use the waiting time to load the next bar or to supervise a second saw. A Horizontal Metal Band Saw Machine with a longer cut time can therefore justify a roller table and a stock rack beside it, because the time saved is spent on handling, not on sawing. A semi-automatic band saw machine fitted this way keeps both the blade and the operator busy.
That brings the numbers back to the shift plan. If the table says a shop needs two saws, it does not need two operators: with 20 to 35 minutes of waiting in every cut, one person can load, set and watch both machines. A second Horizontal Metal Band Saw Machine adds sawing hours far more cheaply than it adds labour, and that is often the deciding point between buying one large saw and buying two.

 +86-13905781129 (wechat) / +86-18767832868
 +86-0578-3559058